Home / Products / Custom Quartz Glass / Thermal Processing
Flame forming, bending, welding, sealing, and annealing of fused silica
Quartz Thermal Processing
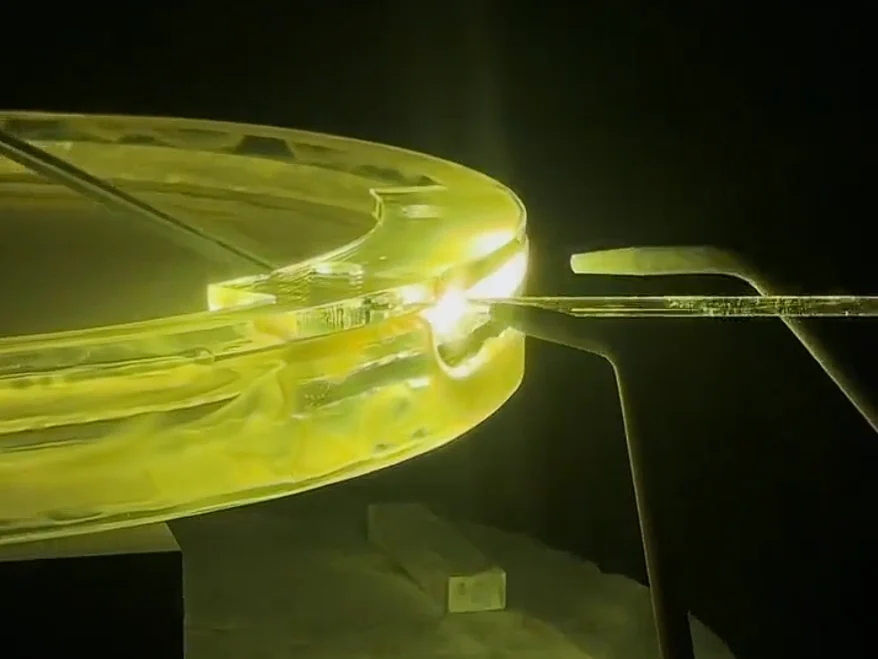
Quartz thermal processing, often called flame working or quartz glassblowing, uses controlled oxy-hydrogen flames to soften fused silica so it can be permanently bent, formed, welded, blown, or sealed without introducing contamination. FGQuartz uses it to build U-bent process tubes, welded multi-port manifolds, hermetically sealed vessels, and multi-chamber assemblies, geometries that CNC machining alone cannot produce.
Flame work is paired with CNC cold processing when a part also needs precise holes, threads, or flat machined faces, as part of custom quartz glass fabrication from a single prototype to production, with no minimum order quantity.
Quick answer
What is quartz thermal processing? The application of extreme, controlled heat, typically from oxy-hydrogen flames, to soften fused silica (softening point near 1680°C) so it can be permanently bent, formed, welded, or sealed.
Key takeaways
- Five core capabilities: forming and profiling, bending, welding, blowing and hermetic sealing, and flame polishing with stress-relief annealing.
- Oxy-hydrogen reaches the temperature fused silica needs and burns clean, producing water vapor rather than contaminants.
- Welds fuse the parent quartz directly with no filler material, so the joint keeps the purity of the base material.
- Welded or heavily formed parts are annealed afterward to relieve stress; opaque fused silica can be formed and welded like clear material.
Written by the FGQuartz Engineering Team · Updated October 2026
On this page: What it is · At a glance · Capabilities · Design guidance · Typical results · Materials · Workflow · Cost drivers · FAQ and quote
Lead time depends on size and drawing complexity; the quote confirms the schedule.
What is quartz thermal processing?
Overview
Quartz thermal processing uses intensely focused, clean-burning oxy-hydrogen flames to heat fused silica past its softening point (about 1680°C). Once plastic, the quartz can be reshaped, stretched, fused, or surface-refined without introducing metallic contamination.
Unlike CNC cold machining, which removes material to drill holes and mill threads, thermal processing changes the structural geometry of the material. Technicians use rotating glass lathes, controlled internal gas pressure, and shaping tools to make clean hollow structures, and every welded or heavily formed part is stress-relief annealed so it survives thermal cycling in service. Forming reshapes a single piece; welding fuses two or more separate components.
Thermal processing vs cold processing: which do you need?
Comparison
| Need | Route |
|---|---|
| A bend, curve, taper, or branch with no straight-line path | Thermal processing — flame forming |
| A sealed, leak-tight joint between two or more pieces | Thermal processing — flame welding |
| A hollow, closed-end vessel or hermetic seal | Thermal processing — blowing and sealing |
| A flat, optically polished surface, or a precise hole or thread | Cold processing — CNC grinding, drilling, milling |
| A tube with a welded side port and a machined flange face | Both, combined — the typical case for complex custom parts |
Housing CNC machining and flame work in one ISO 9001 plant lets FGQuartz fuse machined flanges onto flame-worked assemblies with one drawing and one set of tolerances.
Core thermal processing capabilities
Capabilities
FGQuartz provides a full suite of high-temperature quartz processing, run by experienced technicians on multi-torch glass lathes and precision annealing furnaces.
Thermal processes at a glance
At a glance
Five thermal operations cover almost every flame-worked part. Most parts combine two or more.
| Process | What it does | Typical parts |
|---|---|---|
| Forming and profiling | Reshapes one piece: expands, necks, tapers, thickens. | Transition nozzles, tapered liners, necked tubes. |
| Bending | Curves a tube without adding joints. | U- and L-bends, serpentine process lines. |
| Welding | Fuses two or more parts into one with no filler. | Multi-port manifolds, flanged reactors, side-arm tubes. |
| Blowing and sealing | Makes closed or domed hollow shapes and seals tube ends. | Lamp envelopes, closed-end tubes, reaction vessels. |
| Flame polishing and annealing | Seals surface micro-fissures and relieves internal stress. | Every welded or heavily formed assembly. |
Quartz forming and profiling
Forming reshapes solid rod or tube stock into new geometries. When catalog dimensions cannot meet a design constraint, forming creates custom transitions and necks without adding weld joints.
Capabilities
- Tube reshaping and diameter expansion
- Diameter reduction (necking down)
- Tube collapsing and localized wall thickening
- Smooth tapered transitions and nozzles
- Free-form profiling
How forming works
- The specified zone is heated evenly with an oxy-hydrogen flame on a glass lathe.
- At plasticity, the material is shaped using rotation, graphite tooling, or internal gas pressure.
- Wall thickness is checked with calipers to confirm uniformity.
- The formed profile is stress-relieved to hold dimensional stability.
Typical applications
Specialized CVD process tubes, tapered furnace liners, transition nozzles, and structural elements for semiconductor and optical fiber equipment.
Quartz bending
Thermal bending produces curved tubing while preserving internal surface quality, wall thickness, and transparency. A continuous bent tube has fewer joints than straight sections joined with elbows, which reduces potential leak points and can improve gas flow.
Capabilities
- U-shaped bends
- 90° L-shaped bends
- Custom OEM angles and sweep radii
- Serpentine and multi-direction tubing
Process advantages
- Smooth internal surface with no weld-bead interference
- Fewer mechanical connections
- Better flow and thermal distribution in process systems
- Material purity preserved through the bend
Typical applications
Semiconductor diffusion arrays, laboratory fluid routing, infrared heating loops, and process gas lines in a tight footprint.
Quartz welding
Welding permanently bonds two or more fused silica components by fusing them in an oxy-hydrogen flame. No filler or flux is used, so the seam keeps the purity, chemical inertness, and thermal resistance of the parent quartz. Welding builds complex, leak-tight assemblies such as semiconductor reactor tubes and multi-port process chambers.
Capabilities
- Tube-to-tube butt welding
- Tube-to-plate and flange integration
- Side-port, T-joint, and manifold welding
- Multi-component OEM assemblies
Process
- Mating parts are CNC-machined for alignment and fixtured.
- The joint is heated uniformly until the silica fuses.
- The softened faces are brought together to fuse continuously.
- The weld bead is flame-polished to reduce micro-defects.
- The assembly is stress-relief annealed to help prevent delayed fracture.
Typical applications
Semiconductor process tubes with multi-port gas injection, quartz process chambers, flanged thermal reactors, and multi-branch chemical delivery manifolds. Welds are checked by polariscopic stress inspection and dimensional metrology, and leak-test requirements are agreed per order.
Quartz blowing and hermetic sealing
Blowing creates hollow, thin-walled, or complex closed shapes by combining heat, internal gas pressure, and lathe rotation, expanding silica into spherical or domed forms without weld seams. Sealing closes open tubes or encapsulates internal elements, including flat bases, domed end caps, and closures for sensor protection.
Capabilities
- Seamless, monolithic hollow geometries with few contaminant traps
- Optical clarity retained after forming on clear grades
- Hermetic closure for encapsulated components
Typical applications
UV and IR lamp envelopes, laboratory glassware, closed-end thermocouple protection tubes, and custom reaction vessels.
Flame polishing and stress-relief annealing
Flame polishing sweeps an oxy-hydrogen flame briefly across a machined surface to melt the outermost layer, sealing micro-fissures and restoring a clean, glass-like finish. It reduces particle shedding in cleanroom service and restores transmission on windows.
Stress-relief annealing removes the internal stress that localized heating during forming and welding builds into the silica. Without it, stress can cause failure during thermal cycling.
- The finished assembly is heated into the annealing range (around 1200°C).
- It is held there so internal stress relaxes.
- It is cooled slowly through the strain point so thermal shock is not reintroduced.
Applied to welded multi-port tubes, formed process chambers, heavy-wall crucibles, and any part bound for continuous high-temperature service.
Typical capabilities and achievable results
Typical results
General reference values for the thermal processing lines. Exact results depend on tube diameter, wall thickness, and geometry, and are confirmed in DFM review of your drawing.
| Feature | Typical result |
|---|---|
| Bend radius | Custom and geometry-dependent; wall thickness monitored through the bend |
| Weld integrity | Leak-tight welded joints; weld stress checked by polariscope; leak-test requirements agreed per order |
| Wall thickness during forming | Continuously monitored by caliper |
| Post-weld surface finish | Flame-polished to reduce micro-defects and particle risk |
| Stress relief | Programmed annealing on every welded or heavily formed assembly |
Design guidance for flame-worked quartz parts
Design guidance
General rules that make flame-worked parts easier to build and more reliable in service. Final geometry is confirmed in DFM review.
| Design point | Why it matters |
|---|---|
| Keep wall thickness transitions gradual | Abrupt thick-to-thin changes concentrate stress at the joint and make even heating harder. |
| Mark the critical dimensions | Flame work holds some dimensions more tightly than others. Marking what is functionally critical lets the process route be chosen to protect it. |
| Leave access for the flame and tooling | Weld locations that cannot be reached and rotated on the lathe may need a different assembly sequence. |
| Specify the leak-test requirement up front | Welds are checked for stress and dimensions, and leak-test requirements are agreed per order. |
| Combine hot and cold work early | Features that need machined faces, holes, or threads are planned together with the weld sequence so alignment is preserved. |
| State the service temperature and atmosphere | These decide the grade, the wall, and the annealing needs. |
Common flame-work issues and how they are controlled
Quality control
| Issue | Cause | How it is controlled |
|---|---|---|
| Residual stress | Localized heating during forming and welding. | Stress-relief annealing and polariscope inspection. |
| Wall thinning at bends or expansions | Material stretches as it is formed. | Controlled internal gas pressure and caliper checks during forming. |
| Surface devitrification | Alkali salts or fingerprints on quartz at high temperature. | Clean handling and acid or alcohol cleaning before heat. |
| Incomplete fusion at a joint | Uneven heating or poor alignment. | Machined mating faces, fixturing, and uniform heating, with leak-test requirements agreed per order. |
Materials we process
Materials
Thermal processing works across the same fused silica grades supplied for standard products.
| Grade | Use in formed or welded parts |
|---|---|
| Natural fused quartz | Economical choice for process tubes, bent routing tubes, and general vessels. |
| Synthetic fused silica | Assemblies that also need semiconductor-level purity or optical performance. |
| Opaque fused silica | Formed or welded parts needing thermal insulation or IR blocking, such as furnace liners and heat shields. It forms and welds like clear material. |
| JGS1 / JGS2 optical grades | Blown or sealed vessels and windows needing UV or IR transmission after forming. See the JGS1 / JGS2 / JGS3 guide. |
Describe the application, temperature, and any optical requirement and the engineering team will recommend a grade before quoting.
Our thermal processing workflow
Process
What drives thermal processing cost?
Pricing
Thermal processing pricing depends on four main factors:
- Number of welds and joints. A single bend costs far less than a multi-port manifold with several welded connections.
- Geometry complexity. Tight bend radii, compound curves, and hermetic seals need more technician time and torch setups.
- Wall thickness and diameter. Heavier or larger tubes take longer to heat evenly and form without distortion.
- Order volume. Unit price improves at volume, though single-piece prototypes are accepted with no MOQ.
For an accurate quote, send the drawing with bend angles, weld locations, and critical dimensions marked. Quotations are typically returned within 24 business hours.
Procurement questions
FAQ
Yes. Opaque fused silica can be formed and welded using the same thermal processes as clear material.
Welded assemblies are inspected with polariscopic examination combined with dimensional metrology; leak testing can be arranged for critical applications.
Yes. FGQuartz routinely builds complex thermal assemblies from customer prints and provides DFM feedback.
Fused silica has a softening point near 1680°C — ordinary gas flames cannot reach this temperature, and oxy-hydrogen burns clean.
Forming involves reshaping a single monolithic piece. Welding involves fusing two or more separate components together.
Yes. Through precision lathe-working and flame heating, quartz tubing can be expanded, reduced, tapered, and manipulated into specific geometries.
Quartz welding fuses distinct silica components into complex, seamless, vacuum-tight assemblies like semiconductor LPCVD reactors.
It is the application of extreme, controlled heat (typically via oxy-hydrogen flames) to soften fused silica, allowing it to be permanently bent, formed, welded, or sealed.